
Move your pointer over the image to zoom in
Complete Product Overview
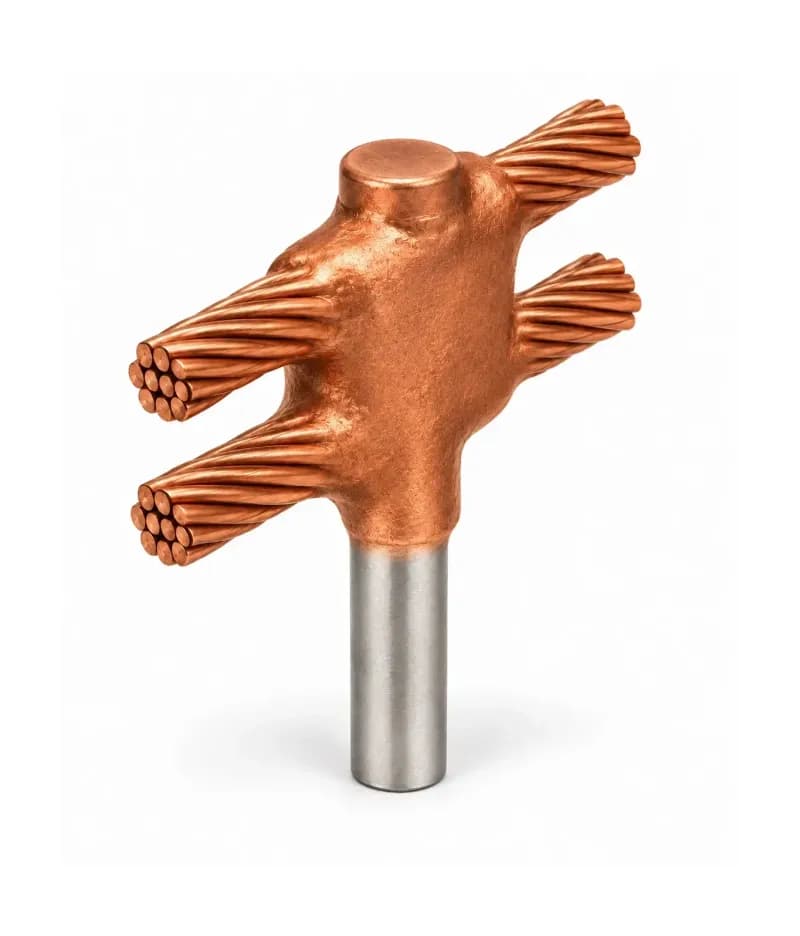
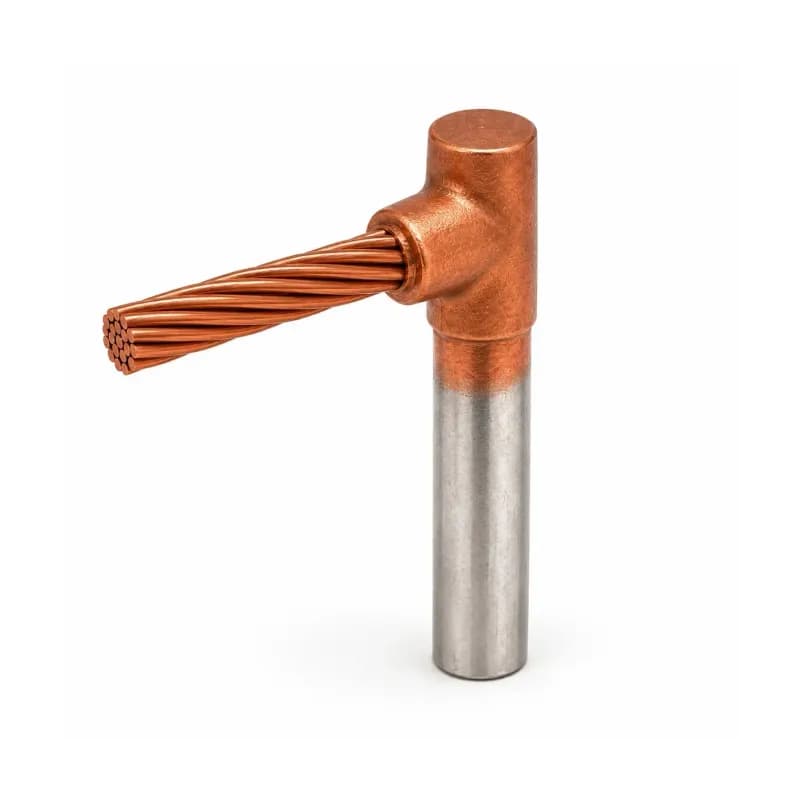
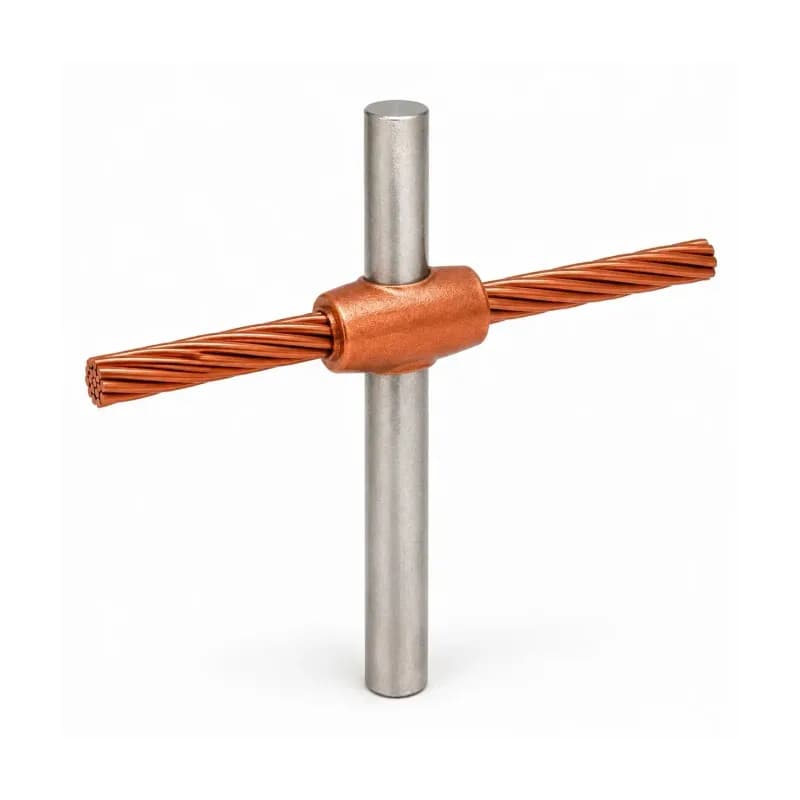
CE2 exothermic weld: through-run copper conductor to the top of an earth rod
Last updated:
The CE2 exothermic weld joins a through-run copper conductor to the top of an earth rod for earthing networks, bonding and lightning protection. We produce its graphite mould under the KALweld® brand and offer it with weld powder and a handle. Once welded, the joint is one piece with the conductors, with no nuts or bolts to work loose over time. KALweld® welds have been tested to IEEE 837 and UL 467 at the Power and Water University of Technology (Shahid Abbaspour) and have passed the freezing, thermal cycling and short-circuit tests.
The CE2 mould is made for 14.2 and 17.2 mm earth rods and 16 to 300 mm² conductors. The mould and powder code for each size is in the "Mould and powder selection" table, and the HC 01 handle fits all its sizes.
Technical Product Information
Click to view enlarged
Mould body material: graphite; mould lid material: stainless steel; suitable handle: HC 01.
CE2 mould and powder selection table
Earth rod diameter (mm) | Thread (inch) | Conductor (mm²) | Weld powder | Mould code |
|---|---|---|---|---|
14.2 | 5/8" | 16 | KWD 090 | CE2-142-016 |
14.2 | 5/8" | 25 | KWD 090 | CE2-142-025 |
14.2 | 5/8" | 35 | KWD 090 | CE2-142-035 |
14.2 | 5/8" | 50 | KWD 090 | CE2-142-050 |
14.2 | 5/8" | 70 | KWD 115 | CE2-142-070 |
14.2 | 5/8" | 95 | KWD 115 | CE2-142-095 |
14.2 | 5/8" | 120 | KWD 150 | CE2-142-120 |
14.2 | 5/8" | 150 | KWD 200 | CE2-142-150 |
14.2 | 5/8" | 185 | KWD 200 | CE2-142-185 |
14.2 | 5/8" | 240 | KWD 250 | CE2-142-240 |
14.2 | 5/8" | 300 | 2 × KWD 150 | CE2-142-300 |
17.2 | 3/4" | 16 | KWD 090 | CE2-172-016 |
17.2 | 3/4" | 25 | KWD 090 | CE2-172-025 |
17.2 | 3/4" | 35 | KWD 090 | CE2-172-035 |
17.2 | 3/4" | 50 | KWD 115 | CE2-172-050 |
17.2 | 3/4" | 70 | KWD 115 | CE2-172-070 |
17.2 | 3/4" | 95 | KWD 115 | CE2-172-095 |
17.2 | 3/4" | 120 | KWD 150 | CE2-172-120 |
17.2 | 3/4" | 150 | KWD 200 | CE2-172-150 |
17.2 | 3/4" | 185 | KWD 200 | CE2-172-185 |
17.2 | 3/4" | 240 | KWD 250 | CE2-172-240 |
17.2 | 3/4" | 300 | 2 × KWD 150 | CE2-172-300 |
The thread on the earth rod top must be cut off before welding.
The CE1, CE2 and CE3 moulds are made for copper-bonded earth rods. For solid copper or stainless steel earth rods, please contact our specialists.
Need another size, or do your conductors not match this table? Send the conductor details or the joint drawing to our specialists and they will recommend the right mould.
Click to view enlarged
Preparing the conductors for conductor-to-earth rod exothermic welding
Cut off the thread on the earth rod top before welding, and flatten any earth rod head that has mushroomed from driving, so the mould sits fully on it. Hold the mould on the earth rod with a clamp so it does not slide down.
Steps
- Check the mould and powder against the table above; the mould code and powder size are also marked on the mould lid.
- Before the first weld, warm a cold mould with a gentle flame to drive off moisture.
- Clean the conductors to bright metal with a wire brush and dry them with a torch.
- Fit the handle on the mould, place the conductors without force in the centre of the weld chamber and lock the mould.
- Place the steel disc at the bottom of the reaction chamber with the concave side up, and gently pour the weld powder over it.
- Sprinkle starter powder over the weld powder and on the edge of the mould, close the lid and light it from the side with a flint igniter, then step away at once.
- Wait at least one minute, open the mould and inspect the weld.
- Clean the slag out of the mould with a soft bristle brush and a scraper; never clean the mould with a wire brush.
See photos of every step, safety notes and the troubleshooting table in the complete illustrated exothermic welding guide, or download the 6-page KALweld® exothermic welding instructions (PDF).
Click to view enlarged
Applications
- Connecting the earth conductor to the top of a copper-bonded or copper earth rod in an earth pit
- Connecting the earth ring to earth rods in substation and building earthing networks
- Permanent below-ground joints that never need to be opened
What does a sound weld look like?
A sound weld fills the mould chamber completely and fully covers the conductors, its slag comes away easily, and after cleaning it has a golden to copper colour. A deep cavity, unmelted conductor under the slag or an incomplete weld means the joint must be welded again.
Test results for KALweld® welds to IEEE 837 and UL 467
KALweld® four-way and T welds on 120 mm² copper conductor were tested at the Power and Water University of Technology (Shahid Abbaspour) (Ministry of Energy) to the IEEE 837 and UL 467 standards, and every test result was "Approved":
Test | Test conditions | Cross weld result (report 95/4221) | Tee weld result (report 95/4220) |
|---|---|---|---|
Freeze-thaw cycle | 10 cycles: more than 2 hours below -10 degrees in water and more than 2 hours above +20 degrees | No cracks or fractures; resistance 176 to 179 µΩ/m (pass) | No cracks or fractures; resistance 179 to 184 µΩ/m (pass) |
Thermal cycle (resistance change) | 25 cycles at a current above 1100 amperes; reference conductor up to 350 degrees | Greatest change in weld resistance 2.8% (pass) | Greatest change in weld resistance 3.0% (pass) |
Weld temperature in the thermal cycle | Thermometer on each weld and on the reference conductor (350 degrees) | 286 to 306 degrees; cooler than the conductor (pass) | 287 to 309 degrees; cooler than the conductor (pass) |
Short circuit (up to melting point) | Circuit of 120 square millimetre copper conductor, 20 kA current | A current of 12 kA was withstood for 8 seconds with no fault; then at 20 kA the copper conductors melted and the welds stayed sound (pass). | At a current of 20 kA the copper conductors melted and the welds stayed sound (pass). |
Full text: report 95/4221, four-way weld, report 95/4220, T weld.
Safety
- Wear heat-resistant gloves, safety glasses and long-sleeved clothing, and move the hot mould only by its handle.
- The mould and conductor must be dry; contact between molten metal and moisture causes spatter.
- After ignition, step back, do not breathe the fumes, and keep combustible materials away from the work area.
- Keep powder and starter in a dry place in undamaged packaging.
Conductors in this joint: copper-bonded earth rod, bare copper conductor.
KALweld® exothermic welding: copper wire to earth rod
Documents & Downloads
Catalogues & datasheets
Certificates & test reports
- Laboratory test report for KALweld® four-way conductor-to-conductor exothermic weld | Power and Water University of TechnologyPersian · 2017-03-14
- Laboratory test report for the KALweld® conductor-to-conductor T exothermic weld | Power and Water University of TechnologyPersian
Installation & application guides
Frequently Asked Questions
What is the CE2 mould code for the smallest size?
For 14.2 / 5/8" / 16, use mould CE2-142-016 with KWD 090 powder. All other sizes are listed in the table on this page.
How many welds can each mould make?
Our moulds are made of high-grade graphite and, used correctly and according to the instructions, last for 50 to 60 welds. Cleaning with a wire brush, knocks, moisture and opening too early all shorten mould life.
After ignition, when should the mould be opened?
Wait at least one minute for the molten metal to solidify, then open the mould carefully.
Which weld powder is right?
The powder size for each conductor size is shown in the table on this page and on the mould lid. Do not substitute powder of another size or another mould.
Have a Technical Question?
KALOT Group's technical experts are ready to answer your questions about lightning rods and earthing systems.